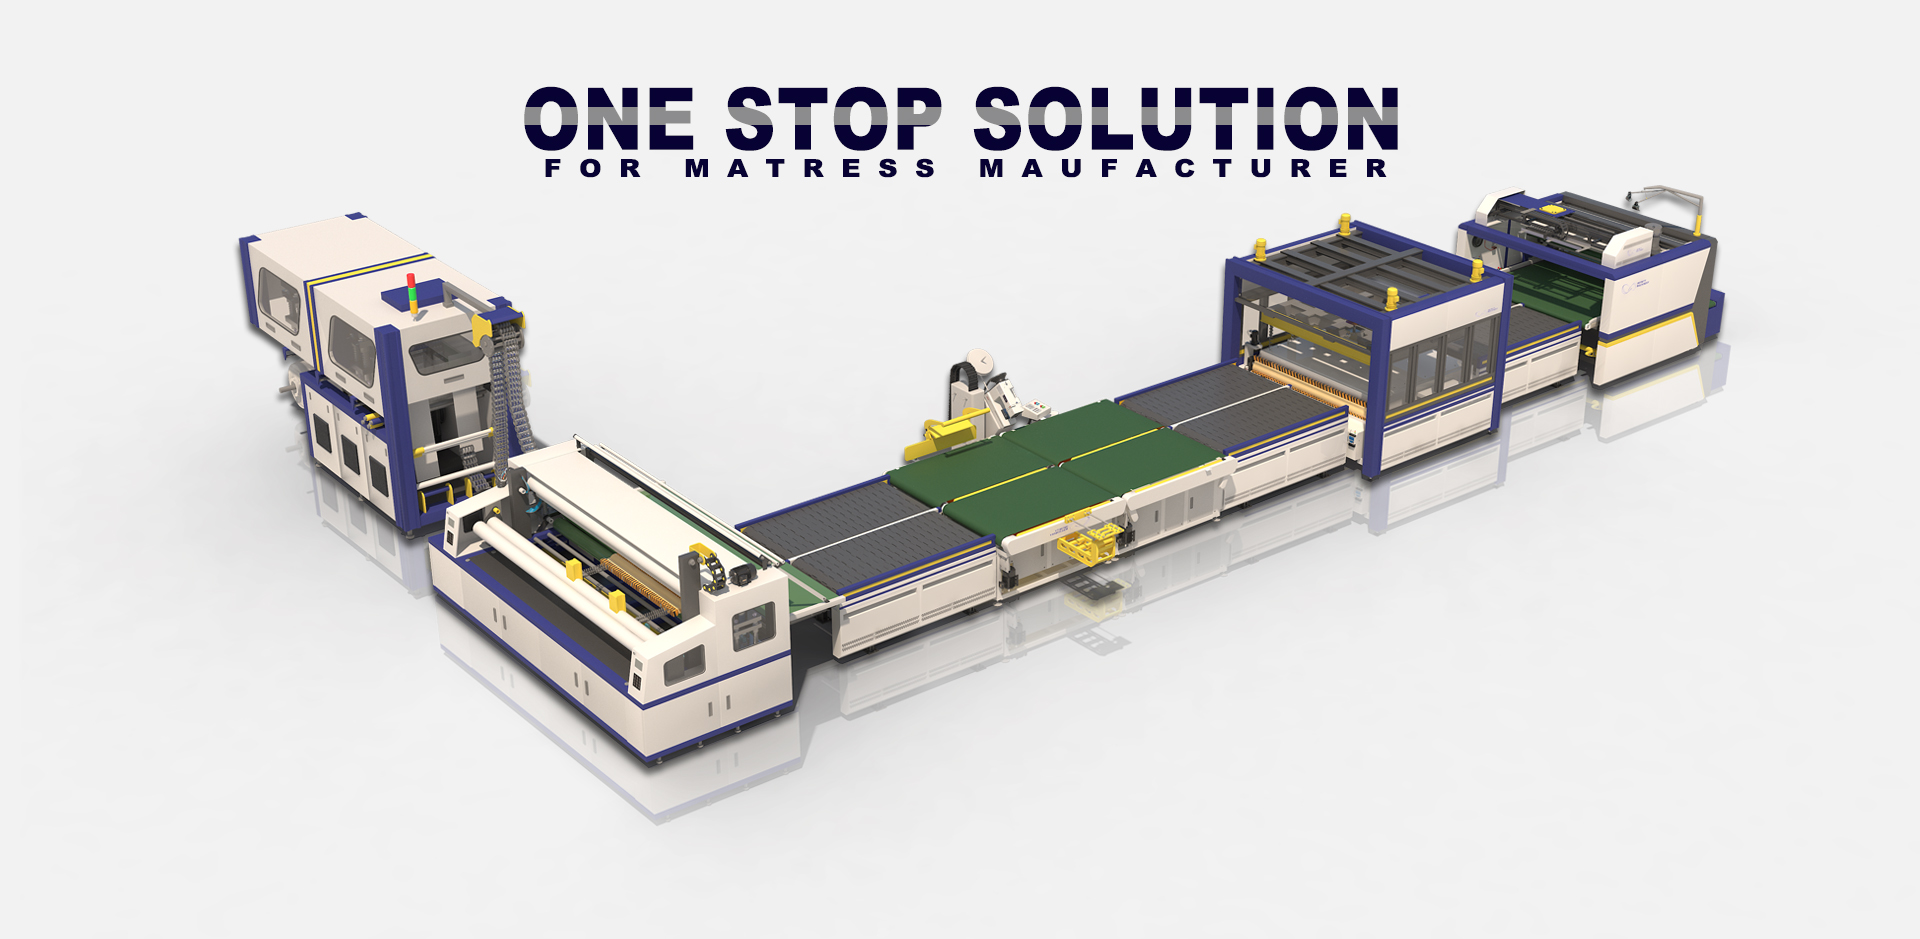
The mattress factory is bought machine by machine, but it has to work as a line: the foaming, the cutting, the quilting, the sewing, the assembly, the tape edge and the packing all feed each other, and the selection mistake in one segment stalls the whole factory. The selection starts with the capacity target, not the machine list: the factory that knows the daily units and the product mix chooses the machines that match the volume, and the factory that buys the machines first builds a line that cannot reach its targets. The IF-APL Mattress Automatic Production Line, the IF-PPA Pocket Spring Assembly and the IF-BCR8 Compress Fold Roll Packaging represent the three automation tiers this guide maps. This guide walks the selection framework from the capacity target to the equipment set.
The mattress factory machinery selection starts with the capacity target, because every machine in the line is sized to a volume. The factory planning number is the daily unit target, the finished mattresses per day, and the target drives the speed and the number of machines in every segment: the cutting capacity must feed the quilting, the quilting must feed the sewing, the sewing must feed the assembly and the assembly must feed the packing. The selection failure modes are three: the over-bought factory, where the machines sit idle because the line cannot feed them; the under-bought factory, where one segment bottlenecks and the whole line waits; and the mismatched factory, where the segments run at different speeds and the work-in-progress piles up between them. The selection framework fixes the three failure modes by planning the line as a flow: the capacity target sets the segment speeds, the segment speeds set the machine specs and the machine specs set the budget. The framework is the same for the 50-unit day and the 500-unit day, only the numbers change.
The capacity target is the anchor: the factory that writes the daily unit number first selects the machines with the segment math, and the factory that skips the number selects on the brochure.
The product mix sits next to the capacity target, because the mattress types use different machines in the same factory. The spring mattress line needs the spring machinery, the pocket spring coiling and assembly, or the Bonnell machinery, and the spring segment is the largest capital line in the factory. The memory foam and the latex lines skip the spring machinery and spend on the foaming and the cutting equipment instead, with the foam production or the foam purchase decision driving the budget. The hybrid factory, the most common in the export markets, runs both: the spring line for the firm mattresses and the foam line for the soft comfort models, sharing the quilting, the sewing and the packing segments. The product mix also sets the panel sizes, the king, queen, double and single, which size the quilting widths and the cutting tables, and the mix ratio, the share of each type, sets the changeover frequency and the flexibility the machines need. The selection rule: the product mix is written as the percentage per mattress type, and the machine set is sized to the dominant type with the changeover flexibility for the rest.
The mattress factory divides into seven segments, and the selection balances them into a flow. Segment one is the material handling: the foam blocks, the fabric rolls and the spring wire arrive and move to the stations, with the storage and the transfer equipment. Segment two is the cutting: the foam block cutting and the panel cutting turn the raw material into the components, with the CNC or the manual machines depending on the volume and the precision. Segment three is the quilting: the fabric panels become the quilted panels, the multi-needle quilting machines for the volume and the single-head for the specialty. Segment four is the spring making: the pocket or the Bonnell line produces the spring units, with the coiling, the assembly and the gluing. Segment five is the assembly and the sewing: the panels, the springs and the comfort layers come together, with the gluing, the border sewing and the tape edge. Segment six is the inspection and the finishing: the finished mattress is checked, the handles and the labels are applied, and the defects are caught before the packing. Segment seven is the packing: the compress, the roll, the film and the carton turn the finished unit into the shippable unit. The selection balances the seven segments at the same speed, because the factory is only as fast as the slowest segment.
The automation level is the third selection variable, and the choice is a labor and capital trade-off across three tiers. Tier one is the manual line: the hand tools and the simple machines, the lowest capital and the highest labor per unit, viable for the small volumes and the low-wage markets, with the quality dependent on the operator skill. Tier two is the semi-automatic line: the machines that automate one operation while the operators load and unload, the middle capital and the middle labor, the standard choice for the mid-volume factory, with the operators becoming the loaders and the quality monitors instead of the hand workers. Tier three is the automatic line: the machines that feed themselves and pass the unit to the next station, the highest capital and the lowest labor per unit, justified by the volume and the labor cost, with the operators running the line instead of working in it. The selection math is the labor comparison: the annual operator cost per station against the capital difference between the tiers, and the payback horizon, typically 18 to 24 months, decides the tier. The factory that selects the tier by the volume instead of the budget builds the line that matches the market.
The machinery selection ends in the budget, and the budget model has four lines. Line one is the capital cost: the machine prices per segment, with the automatic tiers carrying the premium and the semi-automatic the value middle. Line two is the installation and the infrastructure: the floor preparation, the power supply, the compressed air, the dust extraction and the training, which commonly add 15 to 25 percent to the capital number and are the line the new factories underestimate. Line three is the operating cost: the labor, the energy, the maintenance and the consumables per unit, where the automatic tier saves the labor but adds the maintenance and the energy. Line four is the payback: the capital difference between the tiers divided by the annual operating saving, with the 18 to 24 month horizon as the practical selection rule. The phasing plan spends the budget in stages: the phase one machines, the cutting, the quilting and the packing, get the factory running; the phase two machines, the spring line and the automation upgrades, expand the capacity with the revenue; and the phase three machines complete the automatic line. The phased factory buys the equipment the revenue supports, instead of the full set the brochure offers.
Budget lines: capital + installation (15-25% extra) + operating cost + payback | Payback horizon 18-24 months | Phase 1: cutting, quilting, packing | Phase 2: spring line + automation | Phase 3: full automatic line
The roadmap selects the equipment set in six steps, run before the purchase. Step 1: the capacity target, writing the daily unit number and the product mix percentage per mattress type. Step 2: the segment math, sizing the seven segments to the capacity, the speed per segment and the machine count per segment. Step 3: the automation decision, choosing the tier per segment with the labor comparison and the 18 to 24 month payback. Step 4: the layout, placing the machines in the building with the material flow, the buffers and the future expansion space, and confirming the power, the air and the dust infrastructure. Step 5: the budget and the phasing, building the four-line budget and splitting the purchase into the three phases. Step 6: the supplier set, selecting the machinery supplier per segment, verifying the after-sales service, the training and the spare parts, and signing the phased delivery schedule. The factory that runs the six steps gets the equipment set that matches the market volume, the line that flows without the bottleneck and the capital that the revenue supports.
The IF-APL, the IF-PPA and the IF-BCR8 represent the automation tiers this guide maps, and the six-step roadmap selects the full set segment by segment. Contact our factory planning team for the capacity-based equipment proposal for your target volume, the line layout and the phased budget plan.
Contact our factory planning team today for the capacity-based machinery selection: the segment math, the automation tier comparison, the line layout and the phased budget plan for your mattress factory.