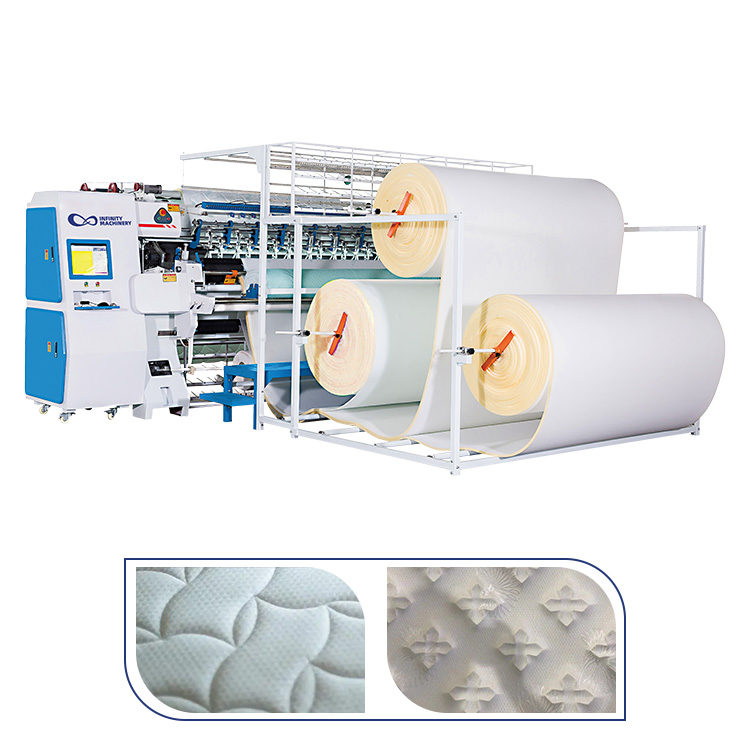
Memory foam quilting runs hot, and the heat is the hidden cause of the failure the line blames on the foam, the thread or the operator. The needle punches through the dense viscoelastic foam hundreds of times a minute, friction heats the needle, and the hot needle melts the foam fibers around the stitch, burns the thread and dulls itself in the same hour. The needle cooling system, air, oil or liquid, keeps the needle below the temperature where the foam softens, and the quilting line that runs the cooling system cuts the rejects, the needle changes and the downtime. The IF-Q-1200 Multi-Functional Quilting Machine, the IF-Q-1300 Multi-Needle Quilting Machine and the IF-Q-1400 Multi-Needle Quilting Machine run the cooling that this guide explains. This guide maps the needle heat problem, the cooling options, the temperature targets and the retrofit plan for the existing line.
The memory foam quilting failure starts where the needle meets the foam, and the cause is heat, not the fabric. The quilting needle punches through the dense viscoelastic foam at high speed, and the friction between the needle shaft and the foam converts the machine energy into heat; the needle tip and shaft climb well above the working temperature during a continuous run. The hot needle does three kinds of damage in the same pass: it melts or burns the foam fibers around the stitch channel, leaving a weak charred hole instead of a clean puncture; it heats the thread and burns the tension, causing the skipped stitches and the thread breaks; and it softens and dulls the needle steel, so the needle wears out in hours instead of days. The line that does not measure the needle temperature blames the failures on the foam batch, the thread lot or the operator, and buys the same failure again with the same settings. The thermal problem is the first variable to control, because the foam, the thread and the needle are all temperature-limited materials.
The needle heat problem is measurable and controllable: the quilting line that tracks the needle temperature sees the failure threshold approaching, and the cooling system holds the needle below the threshold. The failure is not random; it follows the temperature curve of the run.
The needle cooling question is a temperature question, and the numbers set the target. The viscoelastic memory foam softens and begins to deform at roughly 60 to 70 degrees Celsius, and the needle running continuously in the dense foam can reach 90 degrees and above, deep into the failure range; the thread, typically a polyester or nylon, starts to degrade at a similar range, so the needle heat attacks the two materials at once. The practical operating targets are three: the needle stays below 60 to 70 degrees for the memory foam runs, the thread tension stays stable through the full panel, and the stitch channel stays round and clean, without the charred edge that weakens the seam. The cooling system that holds the needle below the threshold converts the failure rate to the normal mechanical rate: the rejects drop, the needle changes drop from hours to days and the thread breaks fall back to the level of the standard runs. The temperature measurement is the control instrument: the infrared thermometer on the needle, or the thermal camera on the needle plate, gives the line the number that the settings and the cooling follow.
Target: needle below 60-70C on memory foam | Foam softens from 60-70C | Failure above 90C | Thread degrades in the same range | Measure with IR thermometer or thermal camera
The needle cooling comes in three system families, and the choice follows the line speed and the foam density. The air cooling system blows a focused jet of compressed air at the needle shaft as it enters the material; the air cooling is the simplest and the cheapest, it works well on the medium-speed lines and the lighter foams, and it doubles as a lint blower that keeps the needle area clean, but it has a limit, because the air removes the heat less efficiently than a liquid and the high-speed dense runs can still push the needle past the target. The oil cooling system circulates a fine oil mist or a drip to the needle, the oil lubricates and cools at the same time; the oil system is common on the industrial sewing and quilting heads, but the oil has to be controlled so it does not stain the light mattress fabrics. The liquid cooling system, the most effective for the dense memory foam, circulates coolant through a cooled needle bar or a cooled sleeve around the needle; the liquid removes the heat continuously and holds the needle at the target through the highest speeds, but it is the most complex and the most expensive to install. The commercial choice is the zone split: air cooling on the light panels and the low-speed stations, oil on the standard heads where the fabric tolerates it, and liquid on the dense memory foam and the high-speed multi-needle runs where the failure cost is the highest.
The needle cooling pays for itself in the stitch quality, and the quality shows in four measurable ways on the finished panel. The first is the clean stitch channel: the cooled needle leaves a round clean puncture, while the hot needle leaves a charred softened channel that tears under the seam stress and shows as a weak spot in the finished mattress cover. The second is the stable thread tension: the cooled thread keeps the consistent tension across the full panel, eliminating the skipped stitches and the loose loops that cluster in the middle of the run when the heat builds; the tension drift is the classic memory foam symptom, the first panels pass and the later panels fail as the needle heats up. The third is the consistent quilting pattern: the machine holds the pattern registration when the needle does not deflect, and the hot softened needle bends under the resistance and shifts the pattern by millimeters. The fourth is the longer needle life: the cooled needle keeps its point and its temper, so the change interval moves from hours to days, and the change downtime disappears from the shift. The panel quality is the direct output: the rejects, the rework and the customer returns all trace back to the needle temperature on the line.
The existing quilting line can be retrofitted with the needle cooling without replacing the machine, and the retrofit plan runs in four steps. Step one is the temperature audit: the line measures the needle temperature on the current memory foam runs, with the IR thermometer or the thermal camera, and records the temperature curve against the run length, the speed and the foam density; the audit shows where the failure threshold is crossed. Step two is the air stage: the compressed air jet kit is the first retrofit, mounted at the needle bar and aimed at the shaft, and the line re-runs the audit to see how far the air cooling closes the gap; the air stage solves the medium-speed lines outright. Step three is the oil or liquid stage: the lines that still cross the threshold at speed upgrade to the oil mist or the liquid sleeve kit on the dense foam stations, with the fabric protection and the drain handling installed. Step four is the operating procedure: the cooling runs on the schedule, the air pressure and the coolant level are on the daily checklist, and the needle temperature is measured weekly as the process control. The retrofit costs a fraction of the new machine, and it converts the failing line to the stable line in the same production week.
The roadmap stabilizes the memory foam quilting line in six steps, run over two production cycles. Step 1: the baseline audit, measuring the needle temperature curve on the current runs and recording the reject, the thread break and the needle change rates. Step 2: the cooling decision, choosing the air, oil or liquid system by the zone, with the dense foam stations on the strongest cooling. Step 3: the installation, mounting the cooling kit, the air supply, the coolant line and the drainage, and verifying the fabric protection on the light panels. Step 4: the process control, setting the temperature target below 60 to 70 degrees and the weekly measurement, and adding the cooling to the daily checklist. Step 5: the re-audit, running the same panels after the installation and comparing the reject, the thread break and the needle change rates against the baseline. Step 6: the standard, documenting the cooling settings per foam type and per speed, and training the operators on the temperature control as part of the shift routine. The line that runs the six steps sees the failure rate drop to the mechanical normal, the needle changes extend from hours to days and the memory foam panels stitch clean across the full run.
The IF-Q-1200, the IF-Q-1300 and the IF-Q-1400 run the needle speed and the cooling that keep the memory foam stitch clean, and the six-step roadmap stabilizes the line without replacing the machine. Contact our quilting team for the needle cooling configuration for your memory foam line, the retrofit kit options and the temperature control procedure.
Contact our quilting team today for the needle cooling configuration for your memory foam line: the air, oil and liquid options, the retrofit kits for the existing machines and the temperature control procedure that stops the failure at the source.